EN



Micro Drill Bits #53–#97 & 1/64"–3/64" — HSS M2 / M35 / M42, 118° Point, ANSI Standard
Number drills #53–#97 (1.511–0.150 mm) and fractional micro drill bits 1/64"–3/64" in HSS M2, M35 (5% Co) and M42 (8% Co). 118° conical point, straight shank, ANSI/ASA B94.11M nominal sizes, bright or black oxide finish. MOQ 500 pcs per size.
- Overview
- Specifications
- Recommended Products
When a hole gets below one millimetre, the drill stops being a disposable consumable and starts being a precision component. This range covers the smallest sizes we make on a production basis — number drills #53 down to #97 and fractional sizes 1/64" to 3/64" — in HSS M2, M35 and M42, ground to US (ANSI/ASA B94.11M) nominal sizes with a 118° point and straight shank. Every size is stocked as a standard catalogue item, not a special order.
Diameter range
0.150 – 1.511 mm
#97 to #53 wire gauge
|
Materials
M2 / M35 / M42
0% · 5% · 8% cobalt
|
Point geometry
118°
135° split point optional
|
Minimum order
500 pcs
per size, mixed sizes allowed
|
What this range is built for
Micro drilling fails for one of three reasons: the bit is eccentric to the spindle, the chip cannot get out, or the tool is too soft for the material. This range is specified to remove all three variables from the tool side of that equation.
Concentric grinding
Point and flutes are ground between centres in one operation, so runout at the point stays inside the tight window these diameters demand. A 0.4 mm bit with 0.02 mm runout is already cutting oversize. |
Polished flutes
Bright-finish flutes reduce friction and chip adhesion at low chip loads. Available in black oxide where you need lubricant retention and better chip flow on gummy materials. |
Cobalt where it matters
M35 (5% Co) and M42 (8% Co) hold hardness at the temperatures microdrilling generates. On stainless and titanium, that is the difference between one hole and forty. |
How small is small
At the bottom of this range the tool is thinner than a human hair. The chart below is drawn to true relative scale against a 0.07 mm hair, so you can judge what you are ordering before you order it.
| Human hair | 0.070 mm | |
| #97 micro drill | 0.150 mm | |
| #79 micro drill | 0.368 mm | |
| 1/64" drill | 0.397 mm | |
| #53 drill | 1.511 mm |
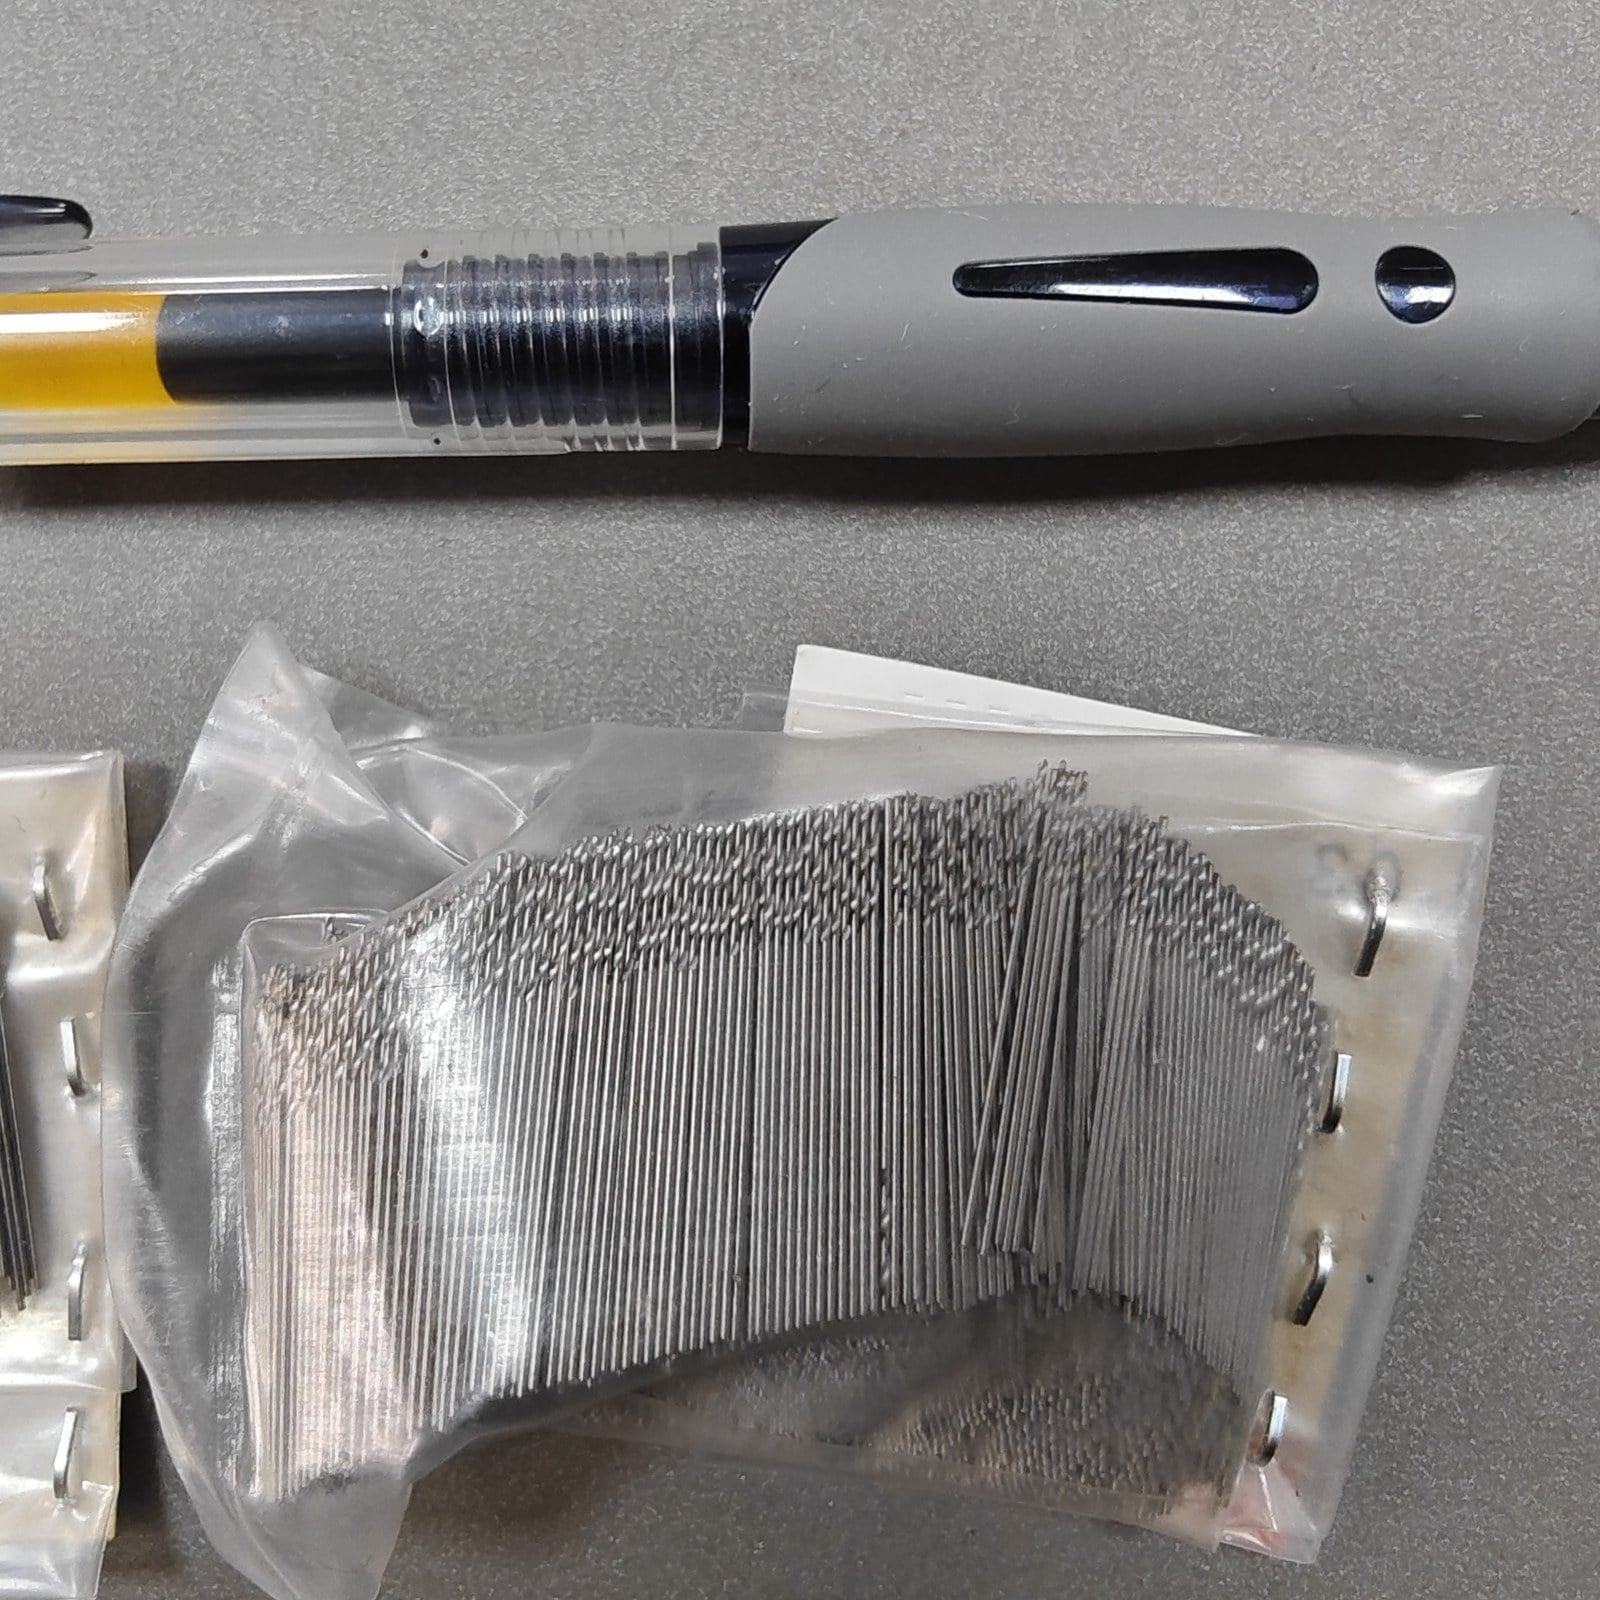
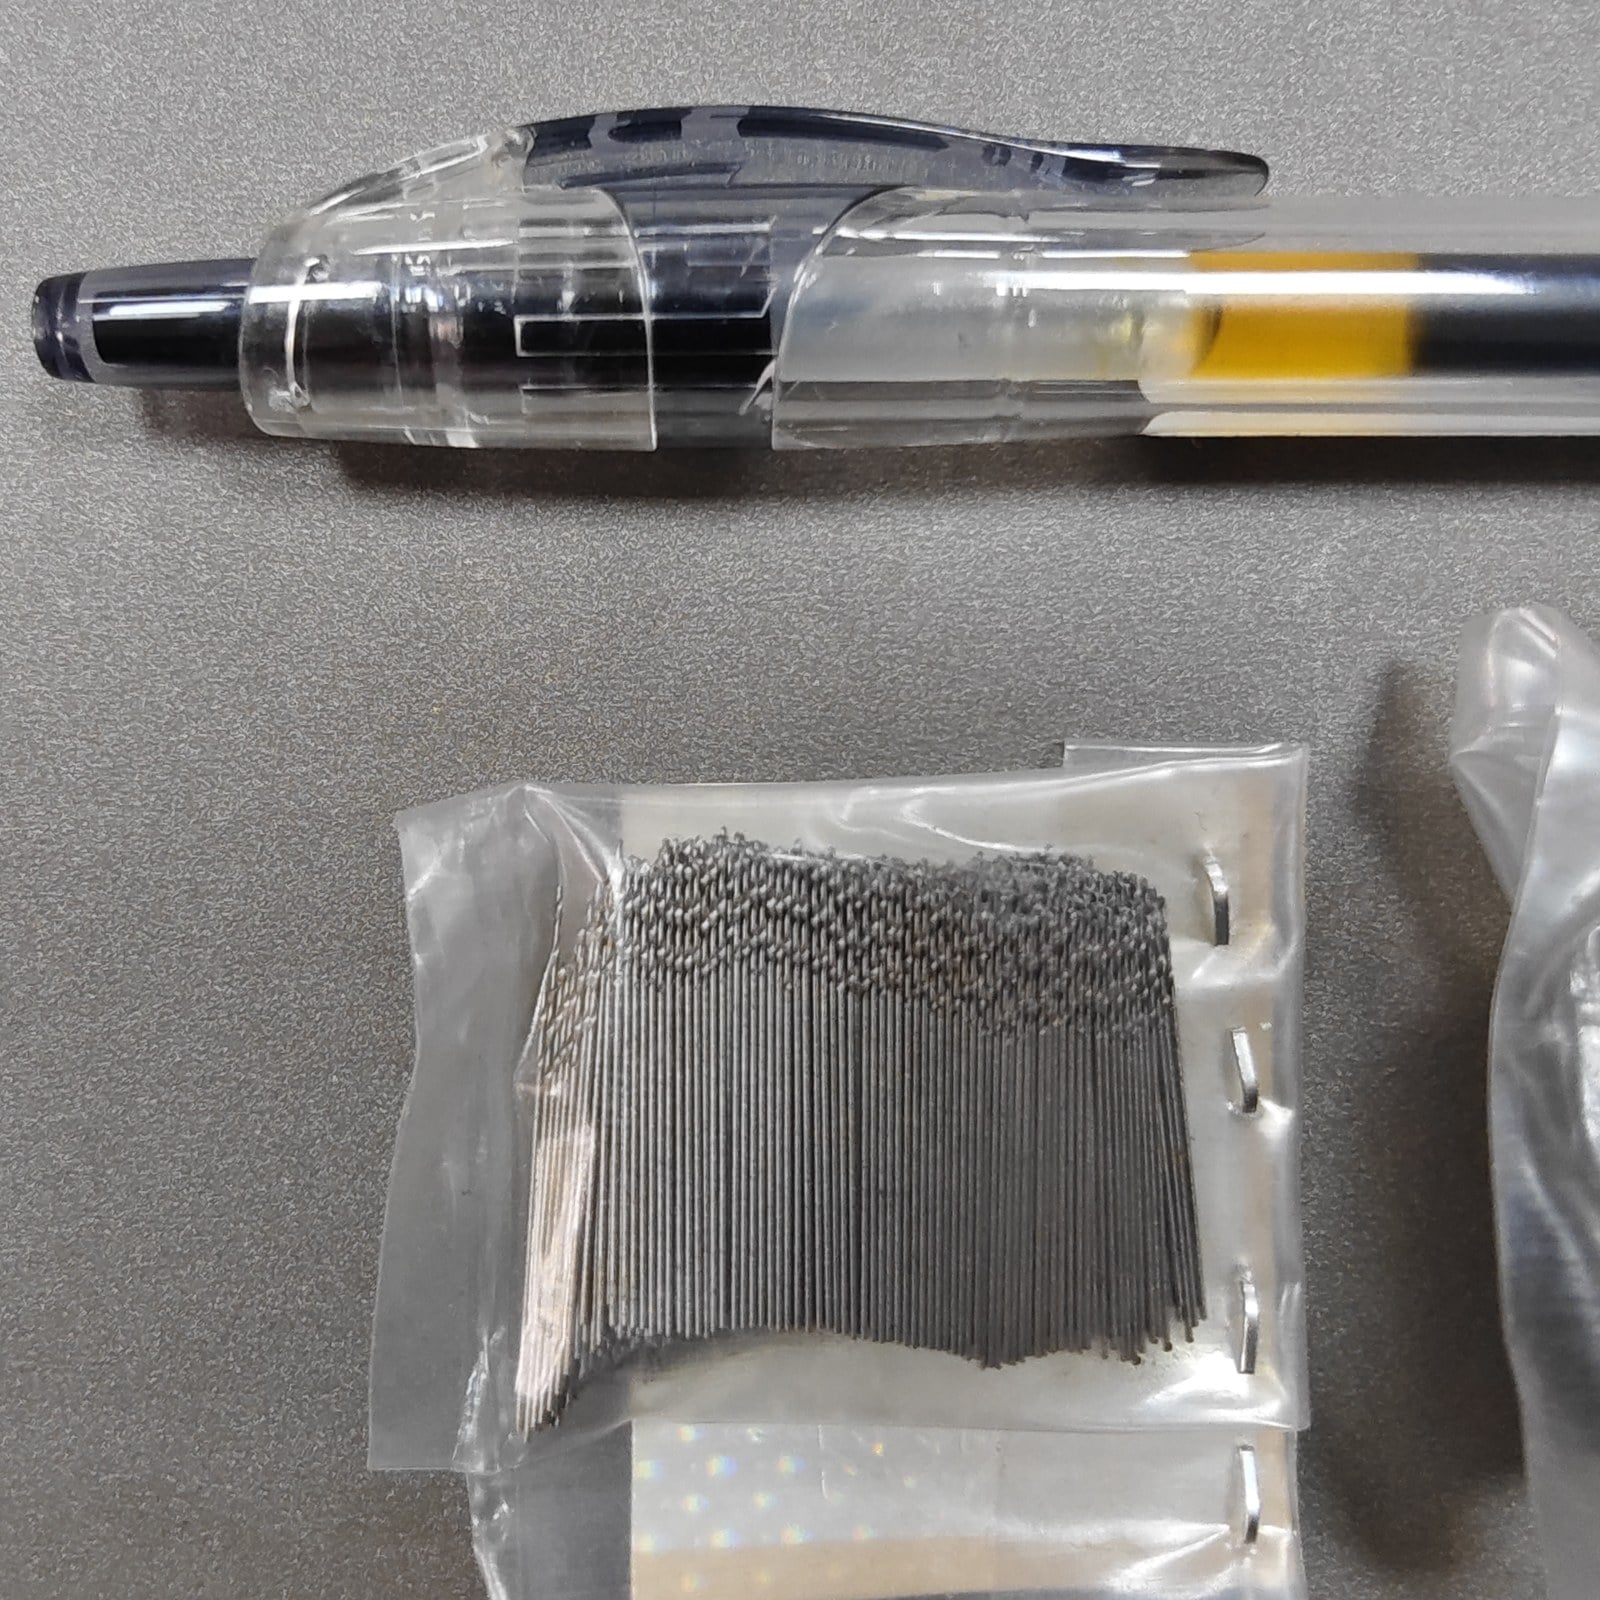
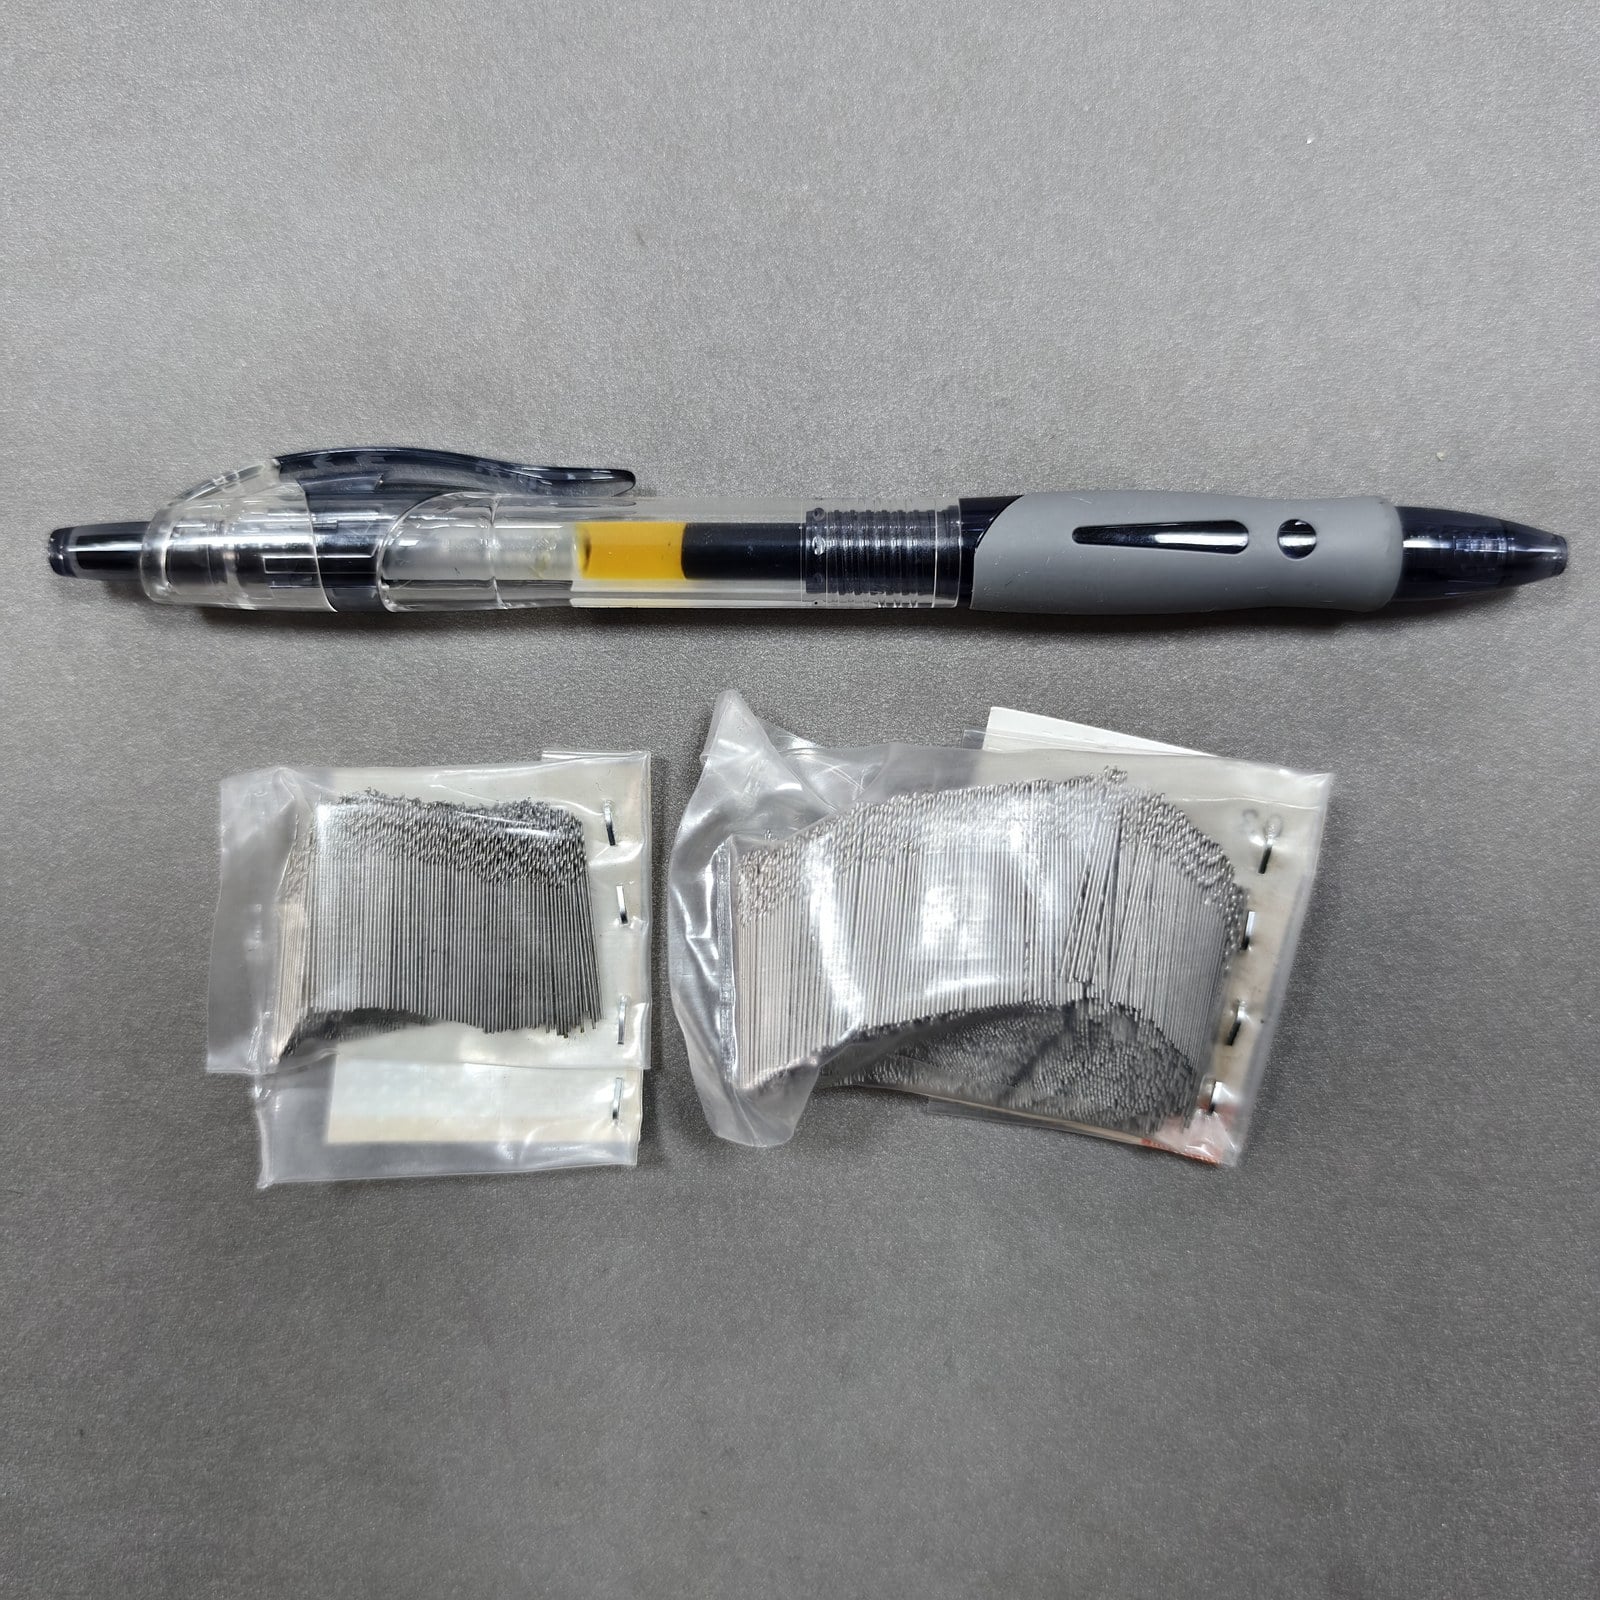
Bars scaled to the largest size in the range (#53, 1.511 mm = 100%). The three photographs below show 1/64" and #79 bits against a ballpoint pen for a physical reference.
 |
 |
 |
M2, M35 or M42 — choosing the grade
All three grades share the same geometry and the same nominal sizes. The difference is cobalt content and the hot hardness it buys you.
| Grade | Cobalt | Typical hardness | Best for | Trade-off |
|---|---|---|---|---|
| M2 | 0% | 63–65 HRC | Aluminium, brass, copper, plastics, wood, mild steel — the general-purpose choice and the most economical per hole | Loses hardness quickly in stainless and high-alloy steel |
| M35 | 5% | 64–66 HRC | Stainless steel 304/316, alloy steel, high-tensile fasteners, production runs where tool changes cost more than the bit | More brittle than M2 — punish it with runout and it snaps |
| M42 | 8% | 65–67 HRC | Titanium alloys, Inconel and nickel-based alloys, hardened tool steel, abrasive composites | Highest cost per piece; demands rigid, high-speed spindles |
Hardness figures are typical values after full heat treatment and apply to the shank body; they are reference values, not acceptance criteria for a specific lot. Tell us the workpiece material and we will recommend the grade and the geometry.
Fractional sizes — 1/64" to 3/64"
Three fractional diameters, each in a standard and a B-series length. The B series extends overall length, which buys you reach in deep cavities and fixture plates.
| Stock No. | Size | Ø mm | Ø inch | OAL mm | Flute mm | OAL inch | Flute inch | Series |
|---|---|---|---|---|---|---|---|---|
| J150097 | 1/64" | 0.397 | 0.0156 | 19.05 | 4.76 | 0.75 | 0.1874 | Std |
| J150098 | 1/32" | 0.794 | 0.0313 | 34.925 | 12.7 | 1.375 | 0.5 | Std |
| J150099 | 3/64" | 1.191 | 0.0469 | 44.45 | 19.05 | 1.75 | 0.75 | Std |
| J150097B | 1/64" | 0.397 | 0.0156 | 28.6 | 4.76 | 1.126 | 0.1874 | B |
| J150098B | 1/32" | 0.794 | 0.0313 | 28.6 | 12.7 | 1.126 | 0.5 | B |
| J150099B | 3/64" | 1.191 | 0.0469 | 38.1 | 19.05 | 1.5 | 0.75 | B |
Dimensions in millimetres per the quoting sheet; inch values converted at 25.4 mm. Stock numbers ending in "B" are a separate production series — overall length differs where shown. Quote by stock number.
Number sizes — #53 to #97
The full wire-gauge run from #53 (1.511 mm) to #97 (0.150 mm). Sizes #61 and finer are produced in the B series; #53 to #60 are available in both series.
| Stock No. | Size | Ø mm | Ø inch | OAL mm | Flute mm | OAL inch | Flute inch | Series |
|---|---|---|---|---|---|---|---|---|
| J160153 | 53 | 1.511 | 0.0595 | 47.62 | 22.225 | 1.8748 | 0.875 | Std / B |
| J160154 | 54 | 1.397 | 0.0550 | 47.62 | 22.225 | 1.8748 | 0.875 | Std / B |
| J160155 | 55 | 1.321 | 0.0520 | 47.62 | 22.225 | 1.8748 | 0.875 | Std / B |
| J160156 | 56 | 1.181 | 0.0465 | 44.45 | 19.05 | 1.75 | 0.75 | Std / B |
| J160157 | 57 | 1.092 | 0.0430 | 44.45 | 19.05 | 1.75 | 0.75 | Std / B |
| J160158 | 58 | 1.067 | 0.0420 | 41.275 | 17.4625 | 1.625 | 0.6875 | Std / B |
| J160159 | 59 | 1.041 | 0.0410 | 41.275 | 17.4625 | 1.625 | 0.6875 | Std / B |
| J160160 | 60 | 1.016 | 0.0400 | 41.275 | 17.4625 | 1.625 | 0.6875 | Std / B |
| J160161B | 61 | 1 | 0.0394 | 41.275 | 17.4625 | 1.625 | 0.6875 | B |
| J160162B | 62 | 0.973 | 0.0383 | 38.1 | 15.875 | 1.5 | 0.625 | B |
| J160163B | 63 | 0.94 | 0.0370 | 38.1 | 15.875 | 1.5 | 0.625 | B |
| J160164B | 64 | 0.914 | 0.0360 | 38.1 | 15.875 | 1.5 | 0.625 | B |
| J160165B | 65 | 0.889 | 0.0350 | 38.1 | 15.875 | 1.5 | 0.625 | B |
| J160166B | 66 | 0.838 | 0.0330 | 34.925 | 12.7 | 1.375 | 0.5 | B |
| J160167B | 67 | 0.813 | 0.0320 | 34.925 | 12.7 | 1.375 | 0.5 | B |
| J160168B | 68 | 0.787 | 0.0310 | 34.925 | 12.7 | 1.375 | 0.5 | B |
| J160169B | 69 | 0.742 | 0.0292 | 34.925 | 12.7 | 1.375 | 0.5 | B |
| J160170B | 70 | 0.711 | 0.0280 | 31.75 | 9.525 | 1.25 | 0.375 | B |
| J160171B | 71 | 0.66 | 0.0260 | 31.75 | 9.525 | 1.25 | 0.375 | B |
| J160172B | 72 | 0.635 | 0.0250 | 31.75 | 9.525 | 1.25 | 0.375 | B |
| J160173B | 73 | 0.61 | 0.0240 | 31.75 | 9.525 | 1.25 | 0.375 | B |
| J160174B | 74 | 0.572 | 0.0225 | 25.4 | 6.35 | 1 | 0.25 | B |
| J160175B | 75 | 0.533 | 0.0210 | 25.4 | 6.35 | 1 | 0.25 | B |
| J160176B | 76 | 0.508 | 0.0200 | 22.225 | 4.7625 | 0.875 | 0.1875 | B |
| J160177B | 77 | 0.457 | 0.0180 | 22.225 | 4.7625 | 0.875 | 0.1875 | B |
| J160178B | 78 | 0.406 | 0.0160 | 22.225 | 4.7625 | 0.875 | 0.1875 | B |
| J160179B | 79 | 0.368 | 0.0145 | 19.05 | 3.175 | 0.75 | 0.125 | B |
| J160180B | 80 | 0.343 | 0.0135 | 19.05 | 3.175 | 0.75 | 0.125 | B |
| J160181B | 81 | 0.33 | 0.0130 | 19.05 | 2.381 | 0.75 | 0.0937 | B |
| J160182B | 82 | 0.318 | 0.0125 | 19.05 | 2.381 | 0.75 | 0.0937 | B |
| J160183B | 83 | 0.305 | 0.0120 | 19.05 | 2.381 | 0.75 | 0.0937 | B |
| J160184B | 84 | 0.292 | 0.0115 | 19.05 | 2.381 | 0.75 | 0.0937 | B |
| J160185B | 85 | 0.279 | 0.0110 | 19.05 | 2.381 | 0.75 | 0.0937 | B |
| J160186B | 86 | 0.267 | 0.0105 | 19.05 | 2.381 | 0.75 | 0.0937 | B |
| J160187B | 87 | 0.254 | 0.0100 | 19.05 | 1.984 | 0.75 | 0.0781 | B |
| J160188B | 88 | 0.241 | 0.0095 | 19.05 | 1.984 | 0.75 | 0.0781 | B |
| J160189B | 89 | 0.231 | 0.0091 | 19.05 | 1.984 | 0.75 | 0.0781 | B |
| J160190B | 90 | 0.221 | 0.0087 | 19.05 | 1.984 | 0.75 | 0.0781 | B |
| J160191B | 91 | 0.211 | 0.0083 | 19.05 | 1.984 | 0.75 | 0.0781 | B |
| J160192B | 92 | 0.201 | 0.0079 | 19.05 | 1.588 | 0.75 | 0.0625 | B |
| J160193B | 93 | 0.191 | 0.0075 | 19.05 | 1.588 | 0.75 | 0.0625 | B |
| J160194B | 94 | 0.18 | 0.0071 | 19.05 | 1.588 | 0.75 | 0.0625 | B |
| J160195B | 95 | 0.17 | 0.0067 | 19.05 | 1.588 | 0.75 | 0.0625 | B |
| J160196B | 96 | 0.16 | 0.0063 | 19.05 | 1.588 | 0.75 | 0.0625 | B |
| J160197B | 97 | 0.15 | 0.0059 | 19.05 | 1.588 | 0.75 | 0.0625 | B |
Starting parameters
Micro bits break from wrong parameters far more often than from bad steel. These are conservative starting points for HSS micro drills — run a test hole, then adjust.
| Workpiece | Cutting speed Vc (m/min) | Feed per revolution | Coolant |
|---|---|---|---|
| Aluminium | 60–100 | 0.02–0.04 mm/rev | Kerosene or soluble oil, flood |
| Brass / copper | 50–80 | 0.02–0.04 mm/rev | Soluble oil |
| Mild / carbon steel | 25–35 | 0.01–0.03 mm/rev | Flood, 8–10% concentration |
| Alloy steel | 18–25 | 0.01–0.02 mm/rev | Flood, high pressure |
| Stainless 304/316 | 12–18 | 0.01–0.02 mm/rev | Flood, never run dry |
| Titanium | 8–12 | 0.008–0.015 mm/rev | High-pressure flood, sharp and copious |
| Hardened steel ≤ 45 HRC | 8–12 | 0.008–0.015 mm/rev | Flood — M42 only |
Spindle speed follows from diameter: n (rpm) = 1000 × Vc ÷ (π × D). A 0.4 mm bit at 30 m/min needs roughly 24,000 rpm — below that you are rubbing, not cutting. Peck in increments of 0.5–1× diameter, keep total runout under 0.01 mm, and hold the bit in a precision collet, never a three-jaw chuck.
Where they are used
PCB & electronicsVia holes, pin holes and component lead clearance in FR4 and phenolic board. |
Jewellery & watchmakingPilot holes for settings, hinge pins and bracelet links in precious and base metals. |
Injection nozzlesOrifice drilling in brass and stainless nozzle tips, where hole size sets flow rate. |
Model & instrument makingFine mechanical assemblies, gauge bodies, camera and optical hardware. |
Aerospace fastenersLockwire holes, rivet pilots and EDM start holes in high-temp alloys. |
Dental & medicalInstrument repair, bur blanks and precision component work. |
Finish, packing and OEM options
| Surface finish | Bright (polished) or black oxide, as standard. TiN and TiAlN coatings available on request for extended life in abrasive materials. |
| Point geometry | 118° conical point as standard. 135° split point available for hard materials and for reduced walking on curved surfaces. |
| Packing | Bulk bag (500 pcs), plastic vial (10 or 100 pcs), or indexed case sets. Tell us the format your shelf and your customers expect. |
| Branding | Laser marking on shank where diameter allows, printed vials, colour-coded caps, private-label artwork and barcoded labels. |
| Documentation | Dimensional inspection data, material certificates and lot traceability available with your order on request. |
Questions buyers ask
Sizes #53–#97 and 1/64"–3/64", M2 / M35 / M42, bright or black oxide, bulk or private label. Volume pricing from 500 pcs per size.
Contact our sales team| Material | HSS M2 / M35 (5% Co) / M42 (8% Co) |
| Standard | ANSI/ASA B94.11M (US standard), nominal sizes |
| Size Range | #53–#97 (1.511–0.150 mm) and 1/64"–3/64" (0.397–1.191 mm) |
| Number of Sizes | 45 wire-gauge + 3 fractional, in standard and B length series |
| Point Angle | 118° conical (135° split point on request) |
| Flute | 2-flute, right-hand cutting, standard helix |
| Shank | Straight (miniature straight shank) |
| Finish | Bright or black oxide |
| Overall Length | 19.05–47.62 mm, by size |
| Minimum Order | 500 pcs per size, sizes may be combined |
| Packing | Bulk bag / plastic vial / indexed case |
| Application | PCB, jewellery & watchmaking, nozzle orifices, model making, aerospace fasteners |