 ×


The general-purpose tap for hand and machine tapping — sold individually or as a 3-piece set
Straight-flute taps cut threads in through holes and blind holes alike, and they are the easiest taps to start by hand. Choose the chamfer type for the job: taper to start a hole, plug for general work, bottoming to thread closest to the bottom.
Straight flutes give the chip a simple, open path — the chip rolls into the flute and is cleared when you back the tap out. There is nothing to clog, which is why this is the design most people mean by "a tap," and why it works in the widest range of materials with the fewest surprises.
Taper chamfer (8–10 threads of lead) — the easiest to start and the most forgiving. Use it to start a hole and to thread through holes by hand.
Plug chamfer (3–5 threads of lead) — the go-to chamfer. A good balance between easy starting and threading depth; works in through holes and blind holes.
Bottoming chamfer (1–2 threads of lead) — cuts threads closest to the bottom of a blind hole. Start the hole with a taper or plug tap, then finish with the bottoming tap.
Sold individually, or as a 3-piece set with one tap of each chamfer type — the practical way to cover a thread size in one purchase.
HSS (high-speed steel), uncoated — the economical, all-purpose choice for maintenance and job-shop work. It holds an edge well in steel, aluminum, brass, and plastic, and can be resharpened. It will dull faster than a cobalt or coated tap in stainless steel and harder alloys.
| Thread size | Thread type | Chamfer | Recommended tap drill | Decimal equiv. |
| 4-40 | UNC | Taper / Plug / Bottoming | 43 ga. | 0.0890" |
| 6-32 | UNC | Taper / Plug / Bottoming | 36 ga. | 0.1065" |
| 8-32 | UNC | Taper / Plug / Bottoming | 29 ga. | 0.1360" |
| 10-24 | UNC | Taper / Plug / Bottoming | 25 ga. | 0.1495" |
| 10-32 | UNF | Taper / Plug / Bottoming | 21 ga. | 0.1590" |
| 1/4"-20 | UNC | Taper / Plug / Bottoming | 7 ga. | 0.2010" |
| 5/16"-18 | UNC | Taper / Plug / Bottoming | F | 0.2570" |
| 3/8"-16 | UNC | Taper / Plug / Bottoming | 5/16" | 0.3125" |
| 1/2"-13 | UNC | Taper / Plug / Bottoming | 27/64" | 0.4219" |
Tap drill sizes above are the standard published values for approximately 75% thread engagement. Flute count runs 3 to 4 depending on thread size. Pitch diameter limit is standard inch-series fit (H2 class). Other thread sizes, left-hand threads, and metric series are available on request.
Prepare the hole — drill with the recommended tap drill, then chamfer the opening so the taper lead has something to bite.
Hold the tap — a tap wrench matched to the shank and square drive end.
Keep it square — a tap guide holds the tap perpendicular for the first few turns — the step that prevents most broken taps.
Steel, cast iron, aluminum, brass, bronze, copper, and most plastics. For stainless steel and harder alloys, a cobalt or coated tap will last longer.
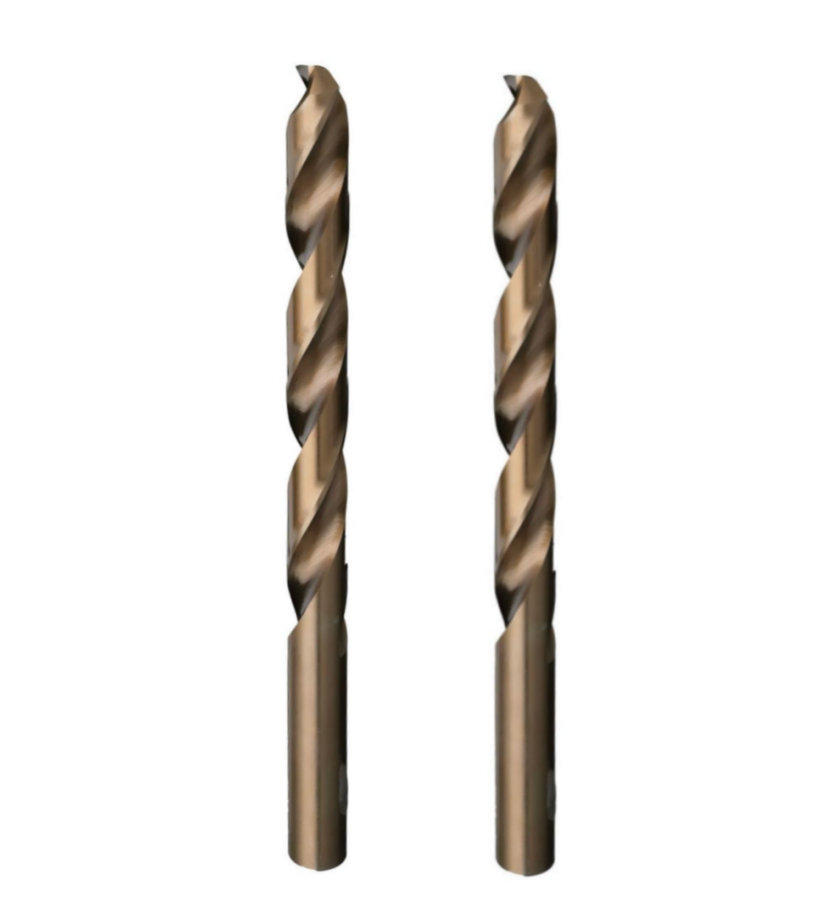
Amsuo Premium Cobalt Heavy Duty Drills - ANSI Standard
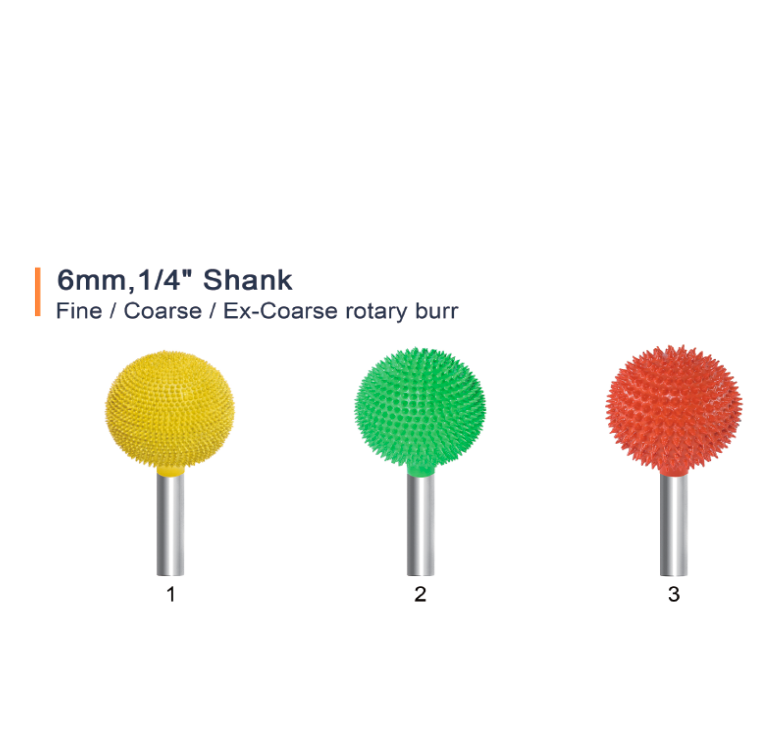
AMSUO Long-Shank Ball Nose Burrs — 8–17 mm, Fine/Coarse/Ex-Coarse
Handheld Armored Thermocouple
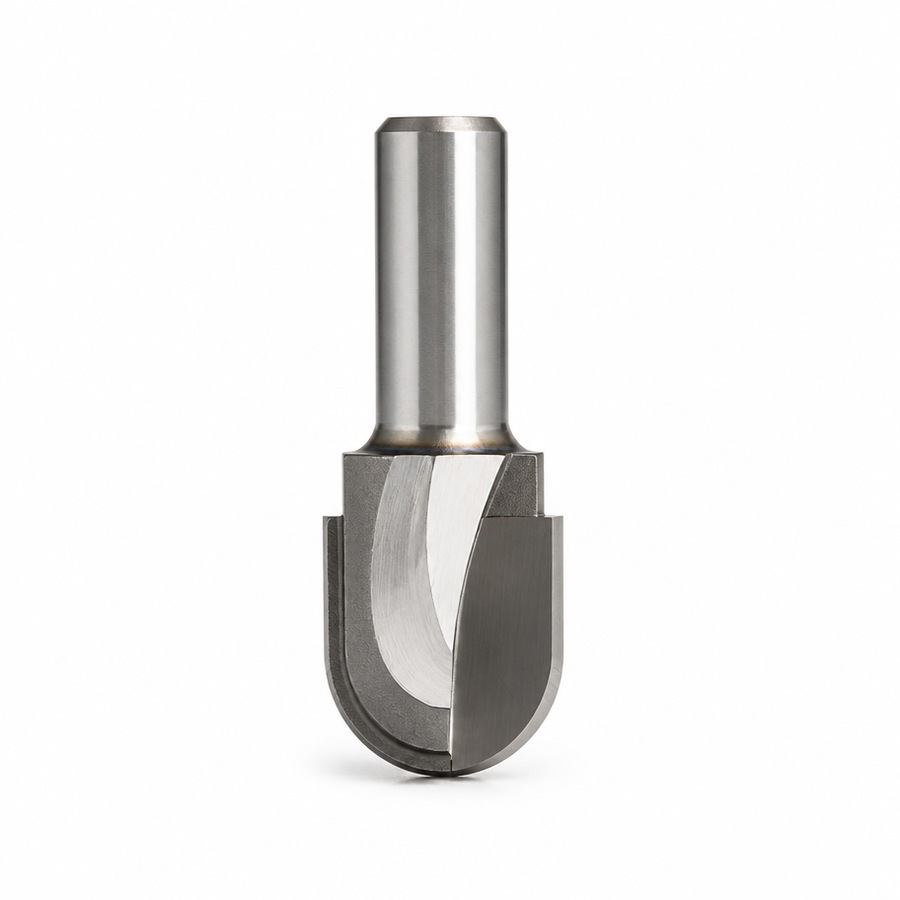
AM031 - Round Nose Router Bit
Copyright © 2026 Amsuo Technology Limited. All rights reserved — Privacy Policy
 EN
