 ×

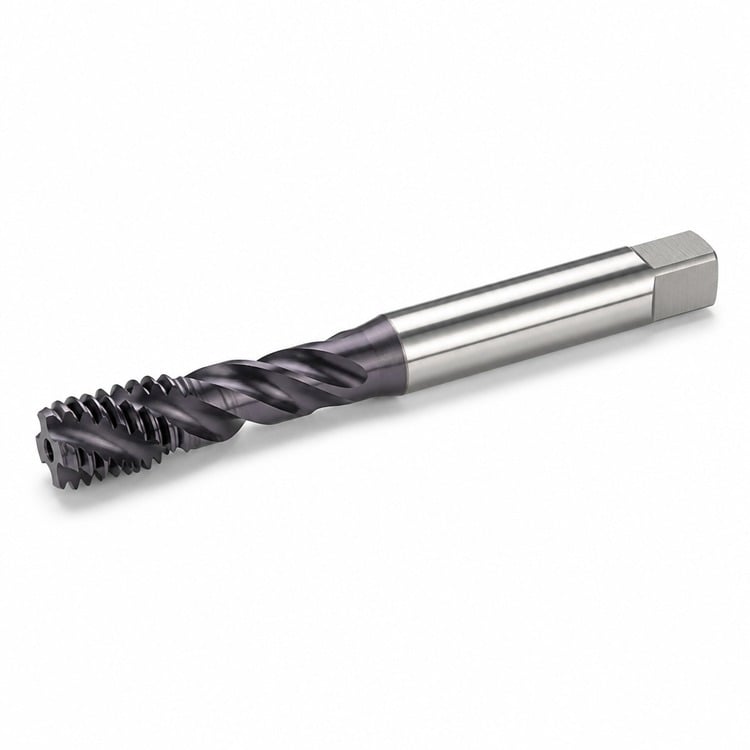
Lift chips back out of blind holes — full thread depth, no packed chips, longer tap life
Spiral-flute taps lift the chip back up and out of the hole as they cut, so a blind hole never fills with packed chips. You get full thread depth all the way down, and you keep the threads and the tap out of harm's way.
The flutes are milled on a helix instead of straight. Turning clockwise, the cutting edges carry the chip up the helix and out of the hole — the opposite direction from a spiral-point tap. That makes these the standard choice for blind holes, where a forward-driven chip has nowhere to go.
HSS-E (cobalt high-speed steel) — resists softening at cutting temperature, which is the main failure mode when a tap cannot be cleared often.
TiCN coating (violet-grey) — titanium carbonitride is harder and more wear-resistant than TiN, making it the usual choice for stainless steel and harder alloys where edge wear drives tap life.
Plug chamfer — the general-purpose lead. Easier to start and easier to turn, but it will not thread as close to the bottom of the hole.
Bottoming chamfer — a shorter lead that cuts threads closest to the bottom of a blind hole. Start the hole with a plug or taper tap, then finish with the bottoming tap.
| Thread size | Thread type | Chamfer | Recommended tap drill | Decimal equiv. |
| 4-40 | UNC | Plug / Bottoming | 43 ga. | 0.0890" |
| 6-32 | UNC | Plug / Bottoming | 36 ga. | 0.1065" |
| 8-32 | UNC | Plug / Bottoming | 29 ga. | 0.1360" |
| 10-24 | UNC | Plug / Bottoming | 25 ga. | 0.1495" |
| 10-32 | UNF | Plug / Bottoming | 21 ga. | 0.1590" |
| 1/4"-20 | UNC | Plug / Bottoming | 7 ga. | 0.2010" |
| 5/16"-18 | UNC | Plug / Bottoming | F | 0.2570" |
| 3/8"-16 | UNC | Plug / Bottoming | 5/16" | 0.3125" |
| 1/2"-13 | UNC | Plug / Bottoming | 27/64" | 0.4219" |
Tap drill sizes above are the standard published values for approximately 75% thread engagement. Flute count runs 2 to 3 depending on thread size. Pitch diameter limit is standard inch-series fit (H2 class). Other thread sizes, left-hand threads, and metric series are available on request.
Prepare the hole — drill to the recommended tap drill depth, allowing extra depth for the chip to collect below the last full thread.
Hold the tap — use a tap wrench matched to the shank and square drive end.
Keep it square — a tap guide keeps the tap perpendicular while the first threads are formed.
Steel, stainless steel, cast iron, aluminum, brass, bronze, copper, and most plastics.
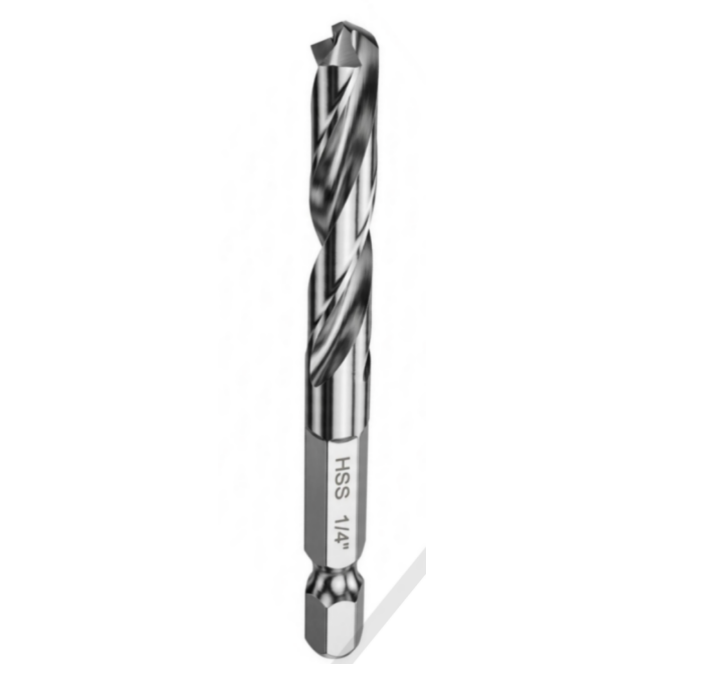
Quick Change Hex Shank Impact Drills/1Pc Design Solid Shank
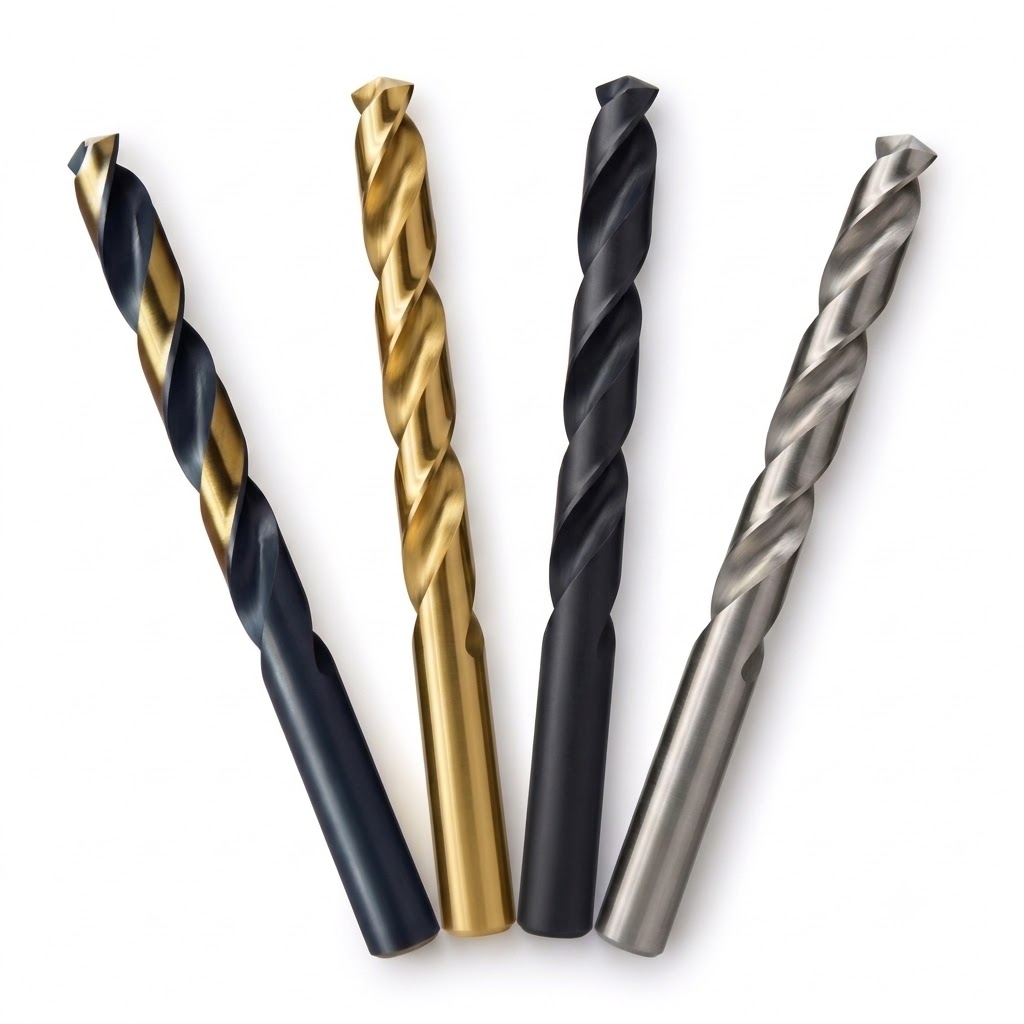
Amsuo Industrial HSS M2 Jobber Drills - ANSI Standard
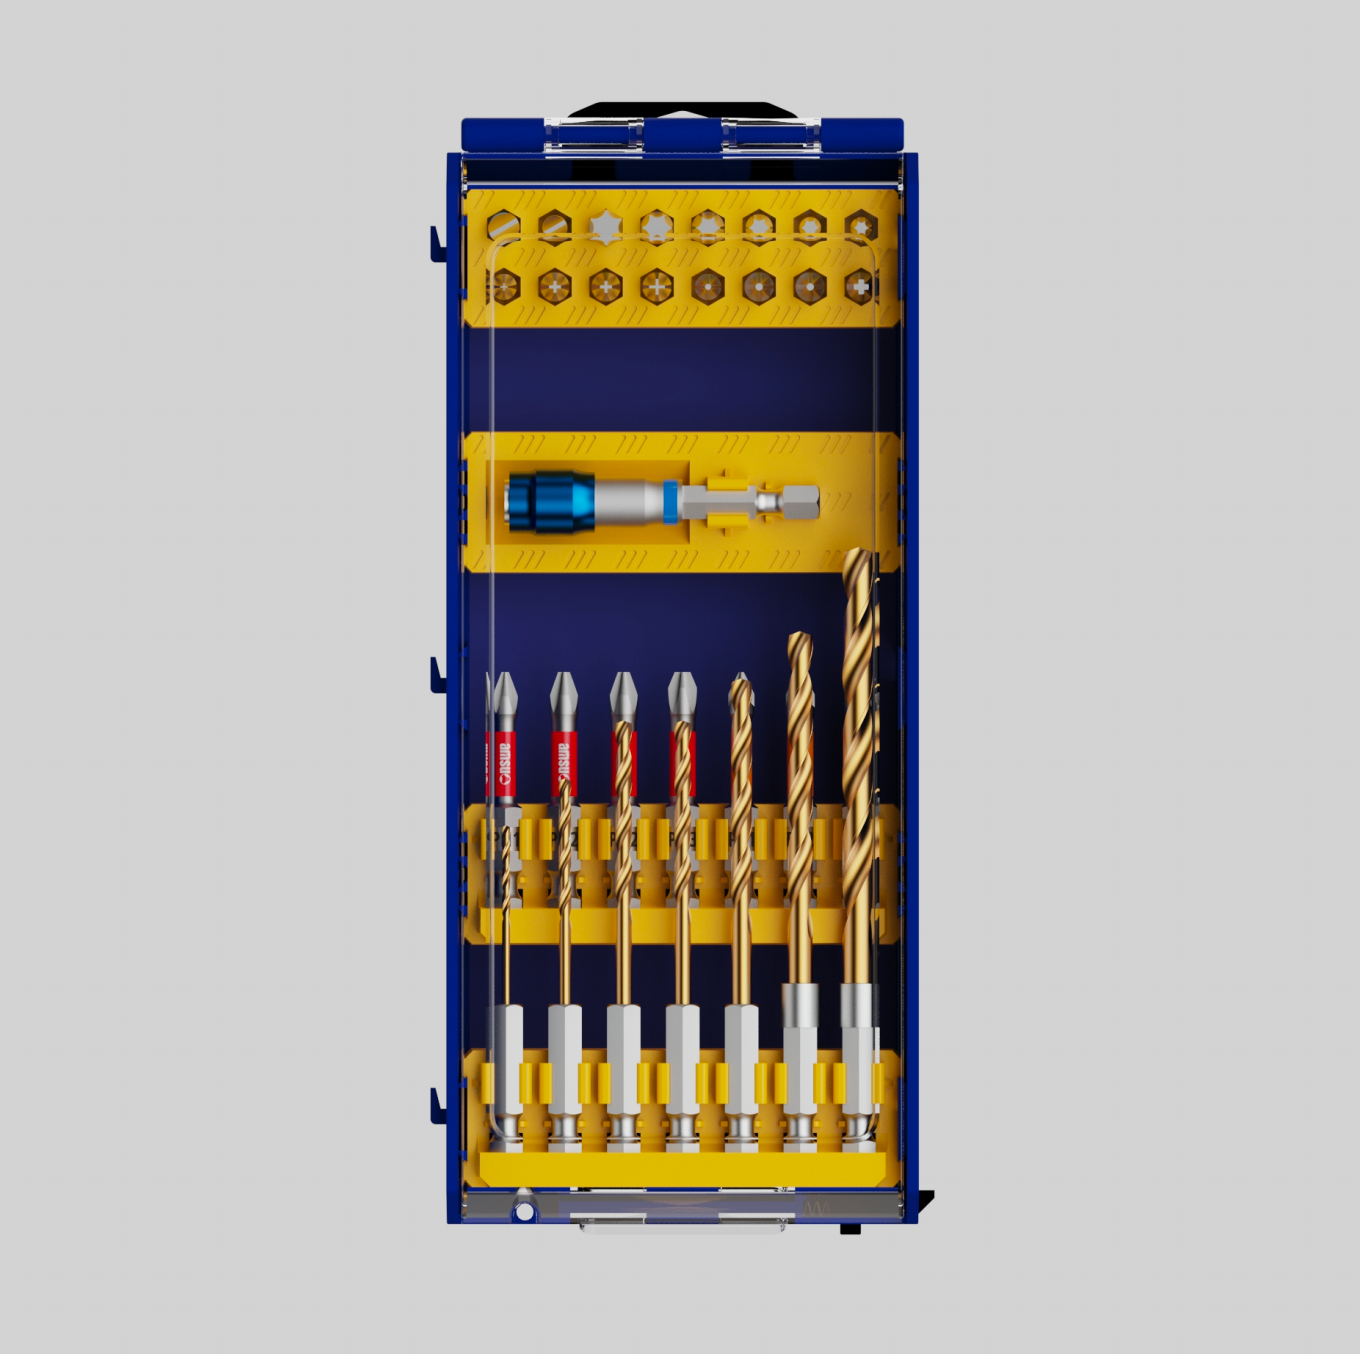
AMSUO 31-Piece Power Bit Set — Bits, Holder & Drill Bits
Temperature Measuring Lance Inner Wire
Copyright © 2026 Amsuo Technology Limited. All rights reserved — Privacy Policy
 EN
