 ×

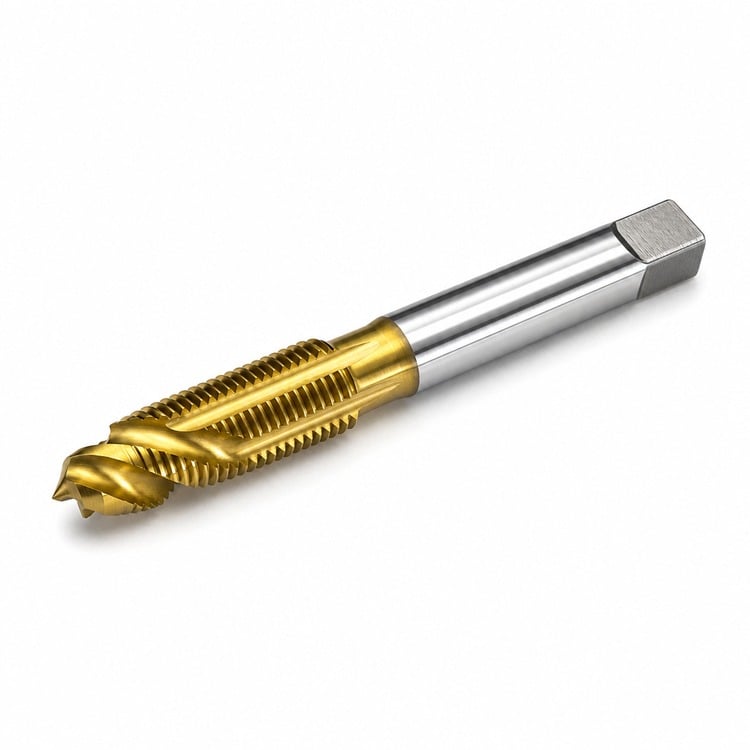
Push chips ahead of the tap and out of the hole — no reversing, cleaner threads, faster passes
Spiral-point taps drive the chip forward and out of the far side of the hole, so you never have to reverse the tap to break or clear it. Threads come out cleaner and the pass finishes faster — this is the tap to reach for whenever the hole goes all the way through.
The tip carries a short ground spiral point that pushes the chip ahead of the cutting edges instead of packing it into the flutes. Also called gun taps, these are the standard choice for through-hole production tapping, whether you drive them by hand or in a machine spindle.
HSS-E (cobalt high-speed steel) — added cobalt raises hot hardness, so the cutting edges hold up in stainless steel and higher-tensile steels where standard HSS softens.
TiN coating (gold) — a hard titanium-nitride layer lowers friction at the cutting edge, which means lower torque, less galling in gummy materials, and a longer service life than an uncoated tap.
| Thread size | Thread type | Chamfer | Recommended tap drill | Decimal equiv. |
| 4-40 | UNC | Plug | 43 ga. | 0.0890" |
| 6-32 | UNC | Plug | 36 ga. | 0.1065" |
| 8-32 | UNC | Plug | 29 ga. | 0.1360" |
| 10-24 | UNC | Plug | 25 ga. | 0.1495" |
| 10-32 | UNF | Plug | 21 ga. | 0.1590" |
| 12-24 | UNC | Plug | 16 ga. | 0.1770" |
| 1/4"-20 | UNC | Plug | 7 ga. | 0.2010" |
| 5/16"-18 | UNC | Plug | F | 0.2570" |
| 3/8"-16 | UNC | Plug | 5/16" | 0.3125" |
| 1/2"-13 | UNC | Plug | 27/64" | 0.4219" |
Tap drill sizes above are the standard published values for approximately 75% thread engagement. Flute count runs 2 to 4 depending on thread size. Pitch diameter limit is standard inch-series fit (H2 class). Other thread sizes, left-hand threads, and metric series are available on request.
Prepare the hole — drill with the recommended tap drill first, then chamfer the opening so the tap starts cleanly.
Hold the tap — a tap wrench sized to the shank and square drive end gives you the leverage to keep the tap turning and the chips moving.
Keep it square — a tap guide holds the tap perpendicular to the surface for the first few turns, which is where most broken taps come from.
Steel, stainless steel, cast iron, aluminum, brass, bronze, copper, and most plastics. For hardened or abrasive materials, a carbide tap is the better choice.
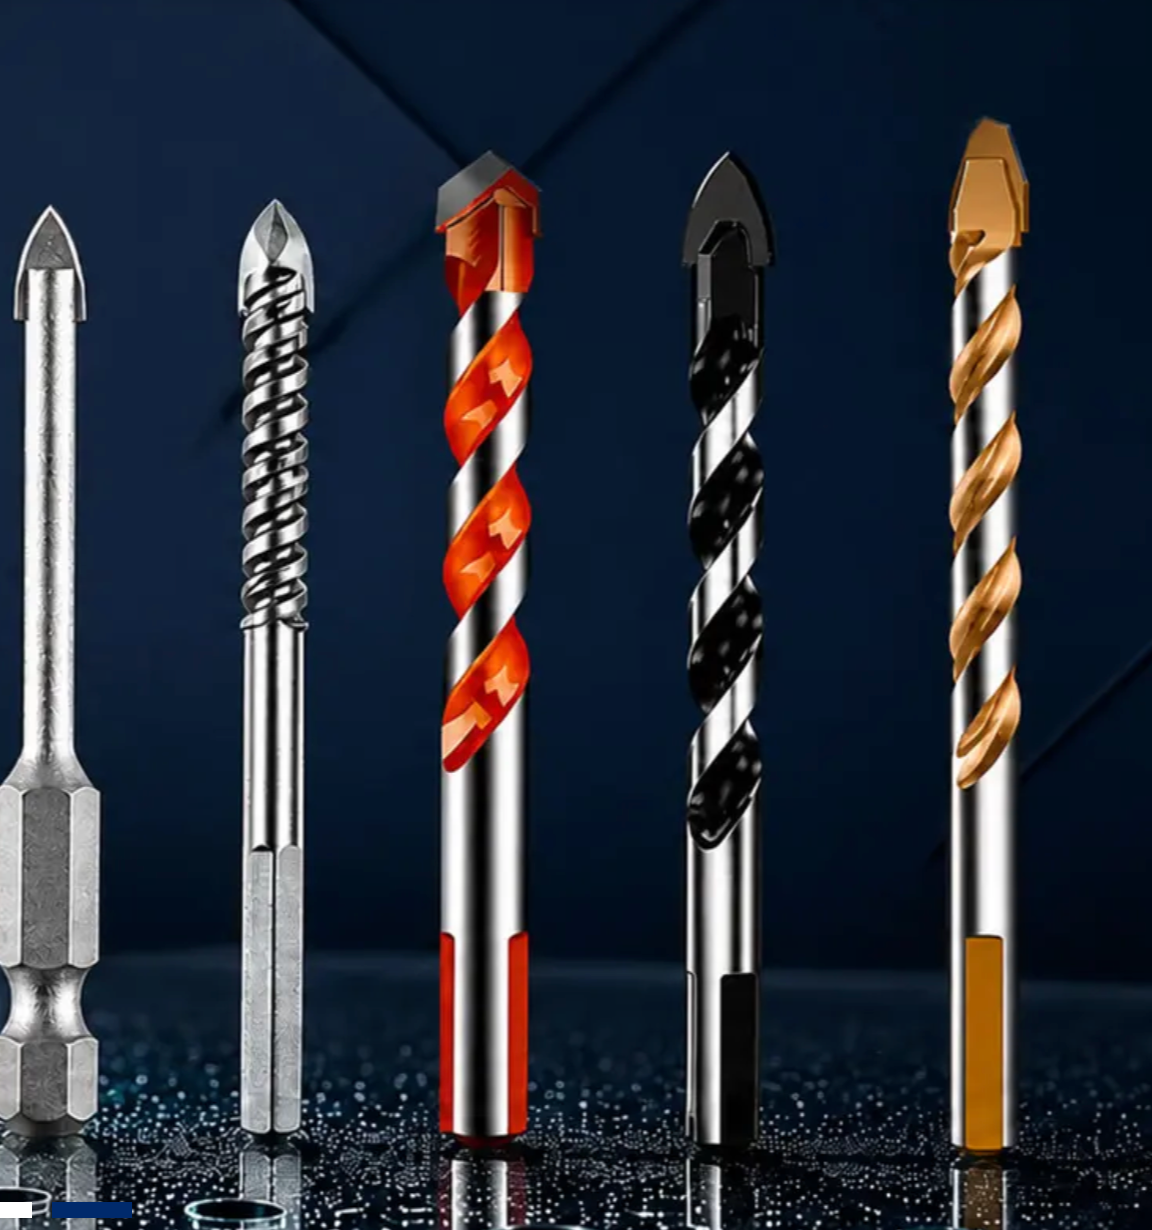
Glass & Tile Drill Bits, 1/4" Hex Shank
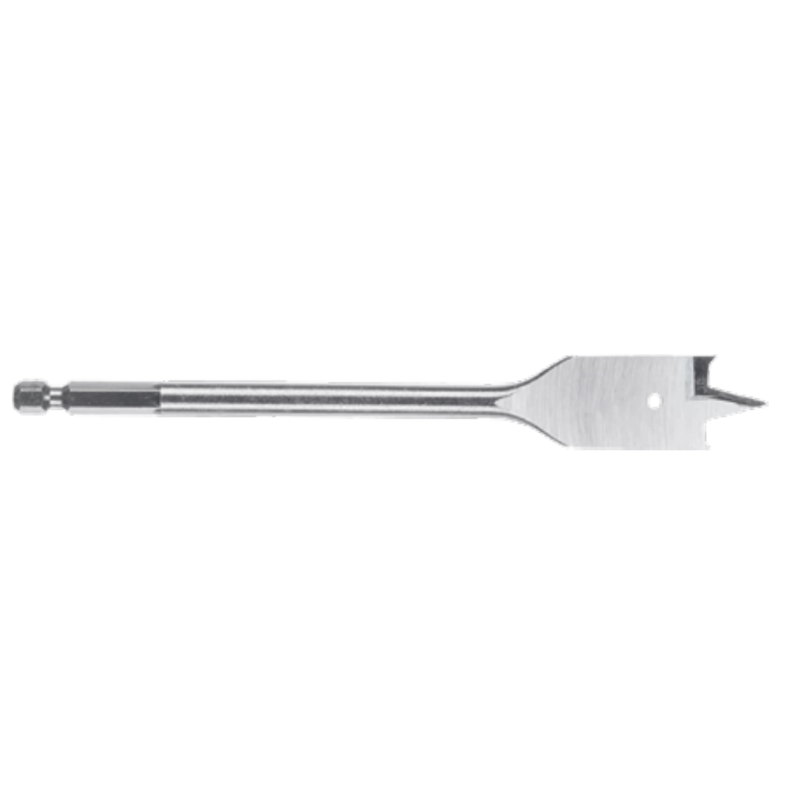
Wood Spade Bit
Socket & Ratchet Wrench Sets

AMSUO Straight-Flute Hand Taps — HSS, Uncoated, UNC Inch Series, Taper / Plug / Bottoming
Copyright © 2026 Amsuo Technology Limited. All rights reserved — Privacy Policy
 EN
